For global packaging buyers, “Rollstock Meaning” is more than a vocabulary question. It describes a continuous packaging web supplied on a roll, ready for forming, filling, and sealing. The material may be plastic film, paper, foil, or a multilayer laminate. Each structure behaves differently on a packaging line. A roll that looks suitable may still fail during sealing, printing, or transport.
This distinction matters because flexible packaging is a large and technically demanding market. Smithers, in The Future of Flexible Packaging to 2028, identifies continued growth in flexible formats, driven by lightweighting, product protection, and convenience. The Flexible Packaging Association also reports that flexible packaging remains important across food, medical, personal-care, and industrial applications. These reports support a practical conclusion: buyers must evaluate performance, not appearance. A clear film for snack packaging is not automatically suitable for products needing high oxygen or moisture protection. Small specification gaps can create large production losses.
Experienced buyers therefore review roll width, gauge, core size, winding direction, seal range, barrier values, print registration, and certification documents. They also confirm whether the rollstock matches the machine’s speed and forming system. That step is often missed. I have seen purchasing discussions focus heavily on price while ignoring changeover time and material waste. This approach needs reconsideration. Regional recycling systems, labeling rules, and shipping conditions can change the best material choice. Reliable sourcing depends on technical data, supplier testing, and traceable quality records—not attractive samples alone. As global packaging expectations evolve, understanding Rollstock Meaning helps buyers ask sharper questions and avoid expensive assumptions.
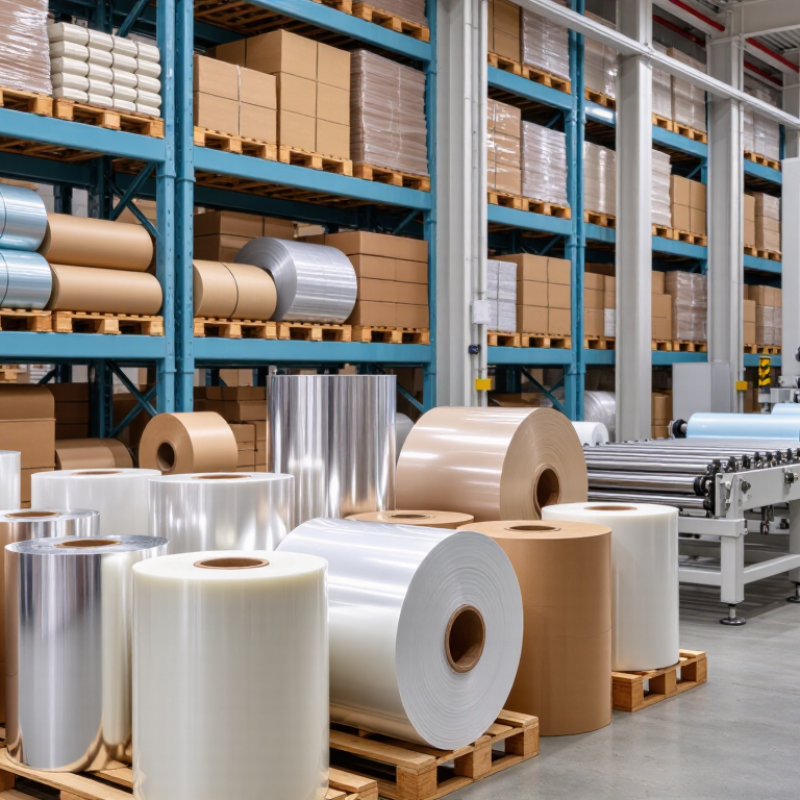
Rollstock means flexible packaging material supplied on a continuous roll. It is not a finished pouch or bag. Converters feed the web through form-fill-seal equipment, then create and seal the package during production.
This distinction changes the buying conversation. A roll may look simple, but its web width, gauge, core size, unwind direction, seal-initiation temperature, and coefficient of friction affect machine performance. Barrier values also matter. Oxygen transmission and water-vapor transmission can influence shelf life, especially for dry foods and sensitive products.
The market is expanding. Smithers’ The Future of Global Flexible Packaging to 2028 projects global flexible packaging demand to exceed US$300 billion by 2028. Flexible formats remain important because they use relatively little material and support efficient transport. However, “lightweight” does not automatically mean better. A thinner film can create seal failures, wrinkles, or line stoppages. That gap matters.
Global buyers should request measurable specifications, not broad descriptions. ASTM F88 can support seal-strength testing, while ASTM F1929 helps assess channel leaks in certain pouch structures. Suppliers should also provide lot traceability, technical data sheets, migration declarations where relevant, and clear storage conditions.
Real purchasing experience shows one recurring problem: samples often run well on one machine but poorly on another. Not always. Humidity, forming temperature, tension control, and operator settings can change the result. Buyers should test production-intent rollstock on the actual filling line before approving large volumes. Packaging machinery market analysis from PMMI also highlights automation and efficiency as major investment priorities, making material-machine compatibility increasingly important.
Rollstock is flexible packaging material supplied in continuous rolls. It is designed for filling, sealing, wrapping, or forming on packaging equipment. Understanding how rollstock is made helps buyers compare specifications accurately. The process usually starts with resin pellets or prepared paper, film, or foil. These materials are extruded, cast, or laminated into a controlled web. The web may then be printed, coated, slit, and wound into rolls. Temperature, tension, and winding pressure affect its final performance.
Rollstock is commonly classified by structure, function, and application. A monolayer film contains one material layer. A multilayer structure combines layers for strength, sealing, printability, or moisture resistance. Some rolls are clear, while others use foil or high-barrier films. Buyers should also check whether the material is intended for vertical form-fill-seal, horizontal form-fill-seal, or thermoforming equipment. Roll width, thickness, core size, and sealing temperature are practical classification details.
In production reviews, I have found that similar-looking rolls can behave very differently. A thinner film may reduce material use but tear during handling. A strong barrier layer may protect contents but complicate recycling decisions. Classification terms can overlap, which creates confusion across markets. That is an imperfect part of international purchasing. Technical data sheets should state layer structure, tolerances, storage conditions, and test methods. Sample trials remain essential because machine settings, humidity, and operator experience can change results. Surface appearance alone is not enough.
Why Rollstock Meaning Matters for Global Buyers?
Rollstock is not simply film on a core. It is a production specification. Global buyers should confirm film structure, thickness, width, roll diameter, core size, and winding direction before ordering. A 60-micron rollstock may run smoothly on one machine but wrinkle on another. Small errors matter.
Barrier data needs equal attention. Ask for oxygen transmission rate, water vapor transmission rate, seal initiation temperature, and hot-tack performance. These values should include test methods, temperature, humidity, and film thickness. Otherwise, comparisons become unreliable. The Flexible Packaging Association’s 2024 industry report valued U.S. flexible packaging sales at approximately $40.9 billion in 2023. That scale reflects a mature market, but it does not remove specification risk.
Printing details can also delay production. Confirm print repeat, registration tolerance, surface treatment, ink compatibility, and unwind orientation. Request a technical data sheet, certificate of analysis, and recent test results. ISO or ASTM references improve traceability. Smithers’ 2024 flexible packaging study identifies downgauging, barrier performance, and material efficiency as continuing market priorities. Lower gauge can reduce material use, yet it may weaken puncture resistance or sealing stability. That trade-off deserves testing, not assumptions. In my experience, buyers often focus on price per kilogram and overlook yield per finished pack. A cheaper roll can create more waste, slower lines, and rejected goods. Ask for evidence.
| Specification Dimension | What “Rollstock” Means | Typical Commercial Range or Requirement | Why Global Buyers Need It | Common Verification Method |
|---|---|---|---|---|
| Material Format | Flexible packaging supplied as a continuous web wound into a roll for forming, filling, and sealing equipment. | Printed or unprinted; mono-material, laminated, coated, or metallized construction. | Confirms whether the material is suitable for vertical, horizontal, or premade pouch production lines. | Technical data sheet and machine trial. |
| Web Width | The usable width of the rollstock across the web direction. | Commonly specified to the forming-collar or machine requirement; tolerance often around ±0.5 to ±1.0 mm. | Incorrect width can cause tracking problems, poor registration, or unusable trim waste. | Calibrated ruler, optical measurement, or supplier inspection report. |
| Total Thickness | The combined thickness of all film, adhesive, ink, coating, and barrier layers. | Typical flexible packaging structures: approximately 40–180 micrometres, depending on application. | Affects stiffness, seal performance, forming behavior, material cost, and package weight. | Micrometer measurement according to ASTM D6988 or an equivalent method. |
| Layer Structure | The ordered combination of sealant, structural, barrier, adhesive, ink, and protective layers. | Examples include PE-based, PP-based, polyester-based, paper-laminated, metallized, or foil-containing structures. | Determines recyclability, barrier level, seal compatibility, puncture resistance, and regulatory suitability. | Layer declaration, cross-section analysis, and supplier compliance documents. |
| Oxygen Transmission Rate (OTR) | The amount of oxygen passing through the packaging material over time. | Approximately <1–10 cm³/m²/day for high-barrier structures; higher values may be acceptable for non-sensitive products. | Important for oxygen-sensitive foods, coffee, pharmaceuticals, and products affected by oxidation. | ASTM D3985 or ISO 15105-2, with temperature and humidity clearly stated. |
| Water Vapor Transmission Rate (WVTR) | The amount of water vapor passing through the rollstock. | Approximately <0.5–5 g/m²/day for high-moisture-barrier structures; application targets vary widely. | Protects moisture-sensitive products such as powders, snacks, dry foods, and hygroscopic materials. | ASTM F1249 or ISO 15106-3, with test temperature and relative humidity stated. |
| Heat-Seal Initiation Temperature | The lowest temperature at which the sealant forms a measurable seal under defined pressure and dwell time. | Often approximately 90–130°C for common heat-sealable flexible structures. | Affects filling speed, energy use, seal integrity, and the risk of product contamination in the seal area. | ASTM F2029 or ASTM F88/F88M seal-strength testing. |
| Seal Strength | The force required to separate a heat-sealed joint. | A practical specification is commonly expressed in N/15 mm or N/25 mm; target values depend on package design and product weight. | Ensures the package remains closed during filling, transport, storage, and handling. | ASTM F88/F88M, with seal temperature, pressure, dwell time, and conditioning recorded. |
| Coefficient of Friction (COF) | The resistance between the film surface and another surface during sliding. | Typical kinetic COF values are approximately 0.20–0.45, depending on the surface and machine design. | Controls film feeding, registration accuracy, slippage, stacking, and machine speed. | ASTM D1894 or ISO 8295. |
| Tensile Strength and Elongation | The film’s resistance to breaking and its stretch before failure in machine and cross directions. | Values vary substantially by polymer and orientation; specifications should list both MD and TD results in MPa and percent. | Indicates resistance to web breaks, stretching, bag deformation, and damage during distribution. | ASTM D882 or ISO 527-3. |
| Roll Diameter and Core | The outside diameter of the wound roll and the internal core diameter used by the converting or packaging machine. | Core sizes commonly include 76 mm and 152 mm; roll diameter is set by machine capacity and shipping limits. | Ensures the roll fits the unwind stand, reduces changeover frequency, and prevents handling issues. | Physical measurement and machine compatibility check. |
| Winding Direction and Unwind | Defines whether the printed or sealant side faces inward or outward and how the web unwinds from the roll. | Must match the packaging-machine unwind direction, print orientation, and sealing configuration. | A mismatch can make the roll unusable without rewinding or machine modification. | Approved winding diagram and line trial. |
| Print Registration | The positional accuracy of graphics, cut marks, eye marks, and other printed features along the web. | Typical registration tolerance is often around ±1 mm, subject to artwork and equipment requirements. | Maintains consistent branding placement, barcode readability, cutting accuracy, and pack appearance. | Artwork proof, repeat-length measurement, and machine inspection. |
| Splices and Roll Integrity | A splice joins two sections of web; roll integrity covers telescoping, wrinkles, blocking, loose edges, and damaged cores. | Splice count, splice position, splice tape, and minimum distance between splices should be agreed before production. | Controls downtime, rejects, web breaks, and operator safety during high-speed packaging. | Incoming roll inspection and documented roll map. |
| Food-Contact and Regulatory Compliance | Documentation confirming that the material is suitable for its intended market and product-contact application. | Declarations should address applicable food-contact, chemical, recycling, labeling, and restricted-substance requirements. | Legal requirements differ by destination market, product type, temperature, and contact conditions. | Declaration of compliance, migration testing, composition statement, and audit records. |
| Storage and Shelf Life | The conditions required to preserve rollstock performance before conversion and filling. | Store in a clean, dry area away from direct sunlight, excessive heat, and moisture; allow temperature acclimatization before use. | Improper storage can cause blocking, curl, adhesive aging, condensation, and unstable sealing. | Warehouse records, packaging inspection, and pre-use conditioning check. |
Note: The numerical ranges shown are general industry reference ranges rather than universal acceptance limits. Final specifications should be confirmed against the product’s barrier needs, packaging-machine settings, destination-market regulations, and agreed test conditions.
Why Rollstock Meaning Matters for Global Buyers?
In packaging procurement, rollstock means a continuous packaging material wound around a core. It may be printed, laminated, coated, or supplied as plain film. This sounds simple. Yet suppliers may use the term differently. For global buyers, that difference can affect material selection, machine performance, and final costs.
The sourcing decision should connect rollstock meaning with production requirements. Buyers need to confirm web width, roll direction, core size, thickness, barrier performance, and sealing temperature. A film that fits one machine may wrinkle or seal poorly on another. Ask for technical data and physical samples. Documents help, but trial rolls reveal curl, tension problems, and waste more clearly. Small details matter.
Price comparisons can also become misleading. A cheaper roll may create higher waste, slower changeovers, or extra testing expenses. Freight volume and roll yield deserve attention too. In practical sourcing reviews, I have seen buyers focus on price before confirming usable output. That approach is understandable, but incomplete. The term rollstock should be defined in writing before quotations are compared. A shared specification reduces confusion between purchasing, engineering, and quality teams. It also supports more reliable supplier evaluation across regions. The process may feel slower at first. It is often less expensive than correcting an unsuitable shipment later.
Rollstock specifications often use different thickness units across markets. A buyer reading “1 mil” should understand that it equals 25.4 microns, while “10 mil” equals 254 microns. Confirming the unit, thickness basis, and tolerance helps prevent incorrect quotations, material substitutions, and sourcing delays.
Conversion basis: 1 inch = 25.4 millimeters exactly; 1 mil = 0.001 inch. Metric thickness values are shown in microns (µm).
Why Rollstock Meaning Matters for Global Buyers?
Rollstock is packaging film supplied on a continuous roll, not a finished pouch. Its value depends on how well it runs on local equipment. The Flexible Packaging Association reported that the U.S. flexible packaging industry reached about $39.5 billion in sales in 2022. This scale shows why buyers need more than a low quotation. Compare seal temperature, film gauge, coefficient of friction, oxygen barrier, moisture barrier, and roll dimensions. These details affect speed, waste, and product protection.
Supplier comparison should also reflect market conditions. Smithers’ global flexible packaging research forecasts continued growth through 2028, driven partly by convenience and lightweighting. However, performance targets differ by region. A humid market may require stronger moisture protection. A distant market may need longer shelf stability and safer transit packaging. Request machine-trial data, migration documentation, quality certificates, and batch traceability. Check whether the supplier can maintain the same structure across plants. Small differences can create large production losses.
Tips: Use a weighted scorecard. Give separate scores for technical performance, compliance, delivery reliability, minimum order quantity, and total landed cost. Ask for three recent production references, but verify them independently. Do not treat a laboratory result as a factory result. No scorecard is perfect; review its weights after every trial. A cheaper rollstock may still be expensive when setup time, rejected rolls, and downtime are included. The best comparison is practical, documented, and slightly skeptical.
Rollstock is flexible packaging material supplied on a continuous roll. It is not a finished pouch or bag. Packaging equipment forms, fills, and seals it during production.
Materials such as film, paper, or foil become a controlled web. The web may be extruded, laminated, printed, coated, slit, and wound. Temperature and tension affect the finished roll.
Confirm web width, thickness, core size, roll direction, sealing temperature, and barrier performance. Check oxygen and moisture transmission when shelf life matters. Small errors can cause large production problems.
Yes. A thin film may reduce material use but tear during handling. Another roll may wrinkle, curl, or seal poorly. Appearance alone tells very little.
Machine settings strongly affect results. Humidity, forming temperature, tension, and operator adjustments can change performance. A sample may run smoothly elsewhere, then fail on your line.
Monolayer film uses one material layer. Multilayer rollstock combines layers for strength, sealing, printing, or moisture resistance. Strong barriers may protect products but complicate recycling decisions.
Not always. A cheaper roll can create more waste, slower changeovers, or extra testing costs. Compare usable output, freight volume, and production speed. Price alone is incomplete.
Request technical data sheets, layer structures, tolerances, storage conditions, and lot traceability. Migration information may matter for product-contact packaging. Documents reduce confusion, but physical trials remain necessary.
Poor compatibility can cause weak seals, wrinkles, leaks, jams, and line stoppages. These problems may appear after a long production run. I sometimes underestimate setup differences; that needs more careful review.
Understanding Rollstock Meaning is essential for global packaging buyers because the term describes flexible packaging material supplied in continuous rolls for later forming, filling, sealing, or converting. Its practical meaning can vary according to the material structure, barrier properties, printing method, and intended application. Rollstock may be classified by substrate, laminate construction, sealing performance, thickness, width, and use conditions. These details help buyers evaluate whether a material is suitable for protecting products, supporting efficient production, and meeting transportation requirements.
A clear understanding of key specifications also improves sourcing decisions. Buyers should compare suppliers based on material consistency, dimensional accuracy, production capability, customization options, quality control, documentation, lead times, and communication efficiency. Comparing offers only by price can create hidden costs when roll dimensions, barrier levels, sealing behavior, or minimum order quantities differ. By defining technical requirements in advance and assessing suppliers using the same criteria, global buyers can reduce misunderstandings, improve supply stability, and select rollstock solutions that match both operational needs and market expectations.
Yuanzhong Printing